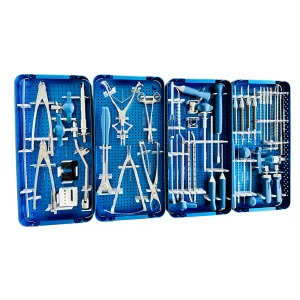
Discover our highly validated, ISO-certified surgical instruments and implants engineered for rigorous clinical requirements.
In modern medicine, wound closure is no longer just about joining tissues; it is a critical process linked directly to postoperative recovery, minimized scarring, and infection prevention. The global market for surgical sutures is witnessing a paradigm shift driven by technological innovations in material science, clinical demands for biocompatibility, and the surging need for highly durable, specialty surgical sutures.
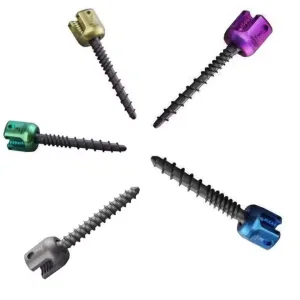
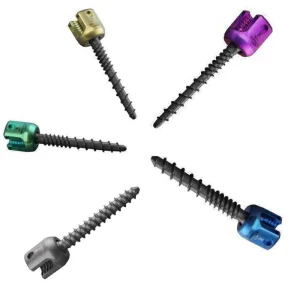
Currently, there is an exponential increase in the demand for absorbable polymeric sutures such as Polydioxanone (PDO), Polyglycolic Acid (PGA), and Poly(glycolide-co-lactide) (PGLA). These materials are highly valued for their predictable absorption profiles and reduced tissue reactivity. Parallel to this, non-absorbable sutures engineered from Ultra-High-Molecular-Weight Polyethylene (UHMWPE) and Titanium/Nickel-Titanium alloys have become the standard in orthopedics, spinal stabilization, and sports medicine. These high-tensile suture systems ensure that high-stress physiological sites remain stable throughout the healing phase, working synergistically with orthopedic implants like spinal pedicle screws and joint replacement configurations.
"The modern surgical landscape demands integration: suture technology must match the longevity, chemical properties, and tensile strengths of adjacent titanium implants and surgical fixation devices."
To ensure patient safety and product efficacy, medical purchasing officers globally prioritize manufacturers who display high-level E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness). As an industry leader in biomedical devices, Shenzhen HUL Healthcare Technology Co., Ltd. (operating under Bopull Medical) excels under this evaluation framework.
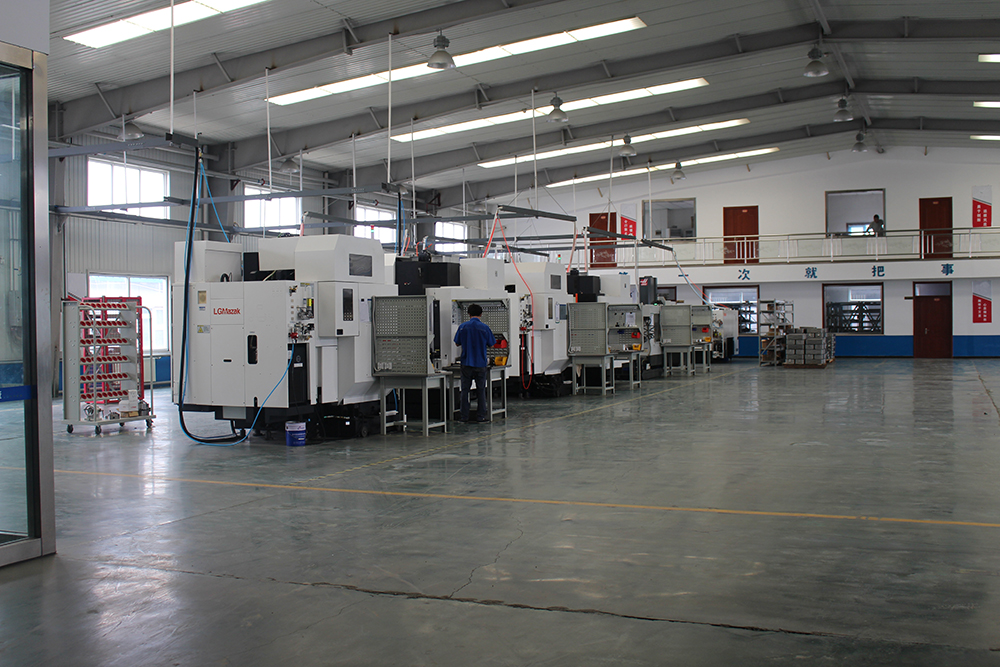
Manufacturing precision medical devices like orthopedic systems and tissue suture accessories requires stringent compliance with international guidelines. Bopull Medical has established an unyielding quality management system certified under GB/T42061-2022 idt ISO13485:2016. This certification demonstrates that from raw material selection to sterile packaging validation, every process is documented and monitored to eradicate defect margins. Our state-of-the-art manufacturing plants leverage automation to guarantee batch-to-batch consistency, providing international partners with reliable, zero-tolerance components for surgical theaters.
The transformation of Chinese industrial parks into Smart Factories (Factory 4.0) has redefine the unit-cost-to-quality ratio in medical device supply chains. By introducing advanced CNC multi-axis milling, automated needle-attaching machines, cleanroom automated packaging, and inline optical quality inspection systems, Chinese manufacturers have achieved unprecedented precision.
At our facilities, cleanrooms operating under Class 10,000 (ISO Class 7) protocols ensure that suture materials, surgical plates, and fixation tools are free from particulate contamination before sterilization. Furthermore, our vertical integration of raw materials—ranging from medical-grade Nitinol wire and premium stainless steel alloys to synthetic biocompatible polymers—insulates global distributors from market volatility. This supply chain resilience is crucial in post-pandemic procurement environments, ensuring consistent lead times and price stability for global distributors and surgical care networks.
Utilizing high-purity medical polymers, titanium alloys, and nickel-titanium wire systems for biocompatible tissue repair and fixation.
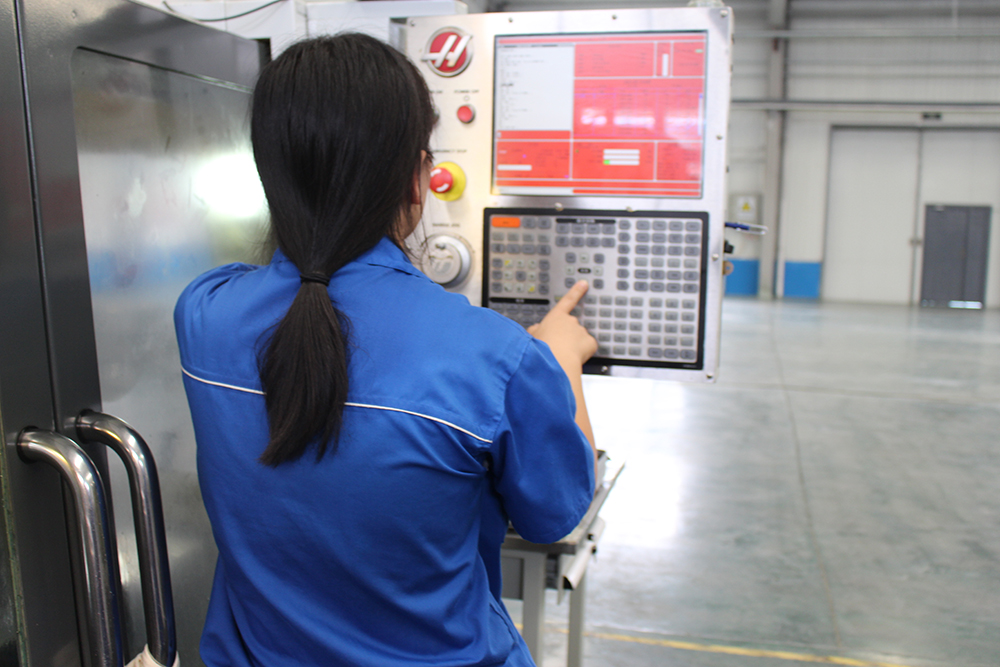
Multi-axis automated machining and assembly minimize human error, achieving micro-level tolerances consistently.
ISO-compliant chemical and gamma-ray sterilization pipelines ensure maximum safety and extended shelf-life.
Medical institutions and surgical instrument distributors face diverse procurement requirements depending on local demographics and regulatory frameworks. In North America and Europe, stringent FDA 510(k) and EU MDR registrations require comprehensive documentation, clinical trial reporting, and trace-back capability. Conversely, in developing healthcare markets, the primary focus lies in balancing robust mechanical performance with cost-efficiency.
Localized Application Scenarios:
Verified profile data for Shenzhen HUL Healthcare Technology Co., Ltd. (Bopull Medical)
Bopull medical has been strictly in accordance with laws and regulations and international standards management and operation, has passed the GB/T42061-2022 idt ISO13485:2016 quality management system international standard certification. Our pursuit of product quality has won high praise in the industry. We purchase advanced equipment, maintain a strong technology infrastructure, and support a young, enterprising, and innovative team with strong professionalism and quality management awareness to provide products that go beyond customer expectations.
| Company Name | Shenzhen HUL Healthcare Technology Co., Ltd. (Bopull Medical) |
| Response Rate | 95.36% |
| Response Time | ≤3h |
| Total Employees | 301 - 500 People |
| Annual Revenue | US$1 Million - US$2.5 Million |
| Seller Reorder Rate | 34% |
| Country / Region | Beijing, China (Trading & Sourcing Division) |
| Business Type | Trading Company with Dedicated Manufacturing Support |
| Year Joined | 3 Years Active |
Engineered for extreme reliability under rigorous orthopedic and bone reconstructive environments.
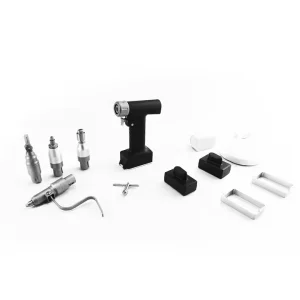
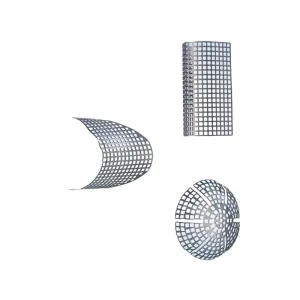
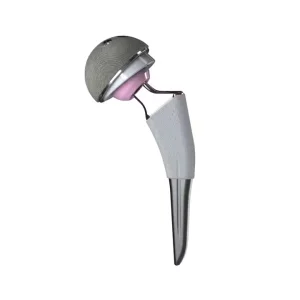
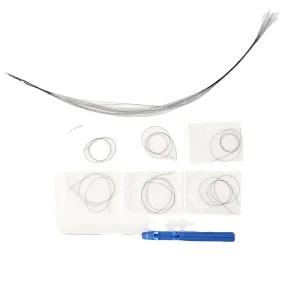
Technical Insights into Medical Materials, Wound Closure, and Surgical Tool Sourcing.
 HUL Healthcare Limited