How our integrated factory processes and material sciences align to produce human-grade and veterinary orthopedic instrumentation of the highest caliber.
We source only high-purity medical alloys including ASTM F136 Titanium and ultra-hard Martensitic/Austenitic Stainless Steel (SUS 316L, 420). This guarantees maximum biocompatibility, high tensile strength, and corrosion resistance under aggressive autoclaving conditions.
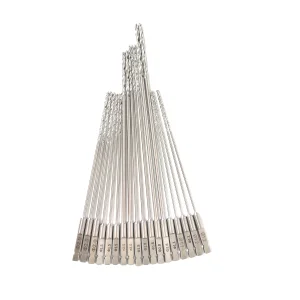
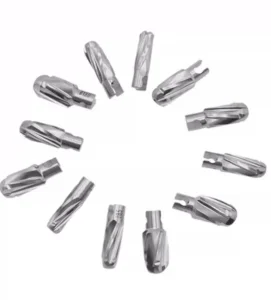
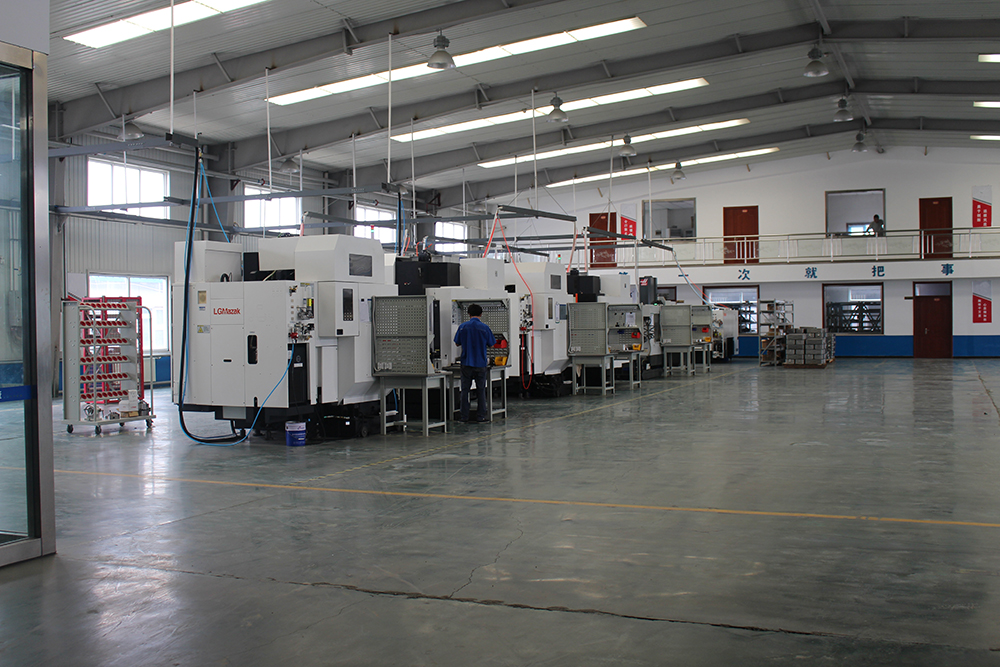
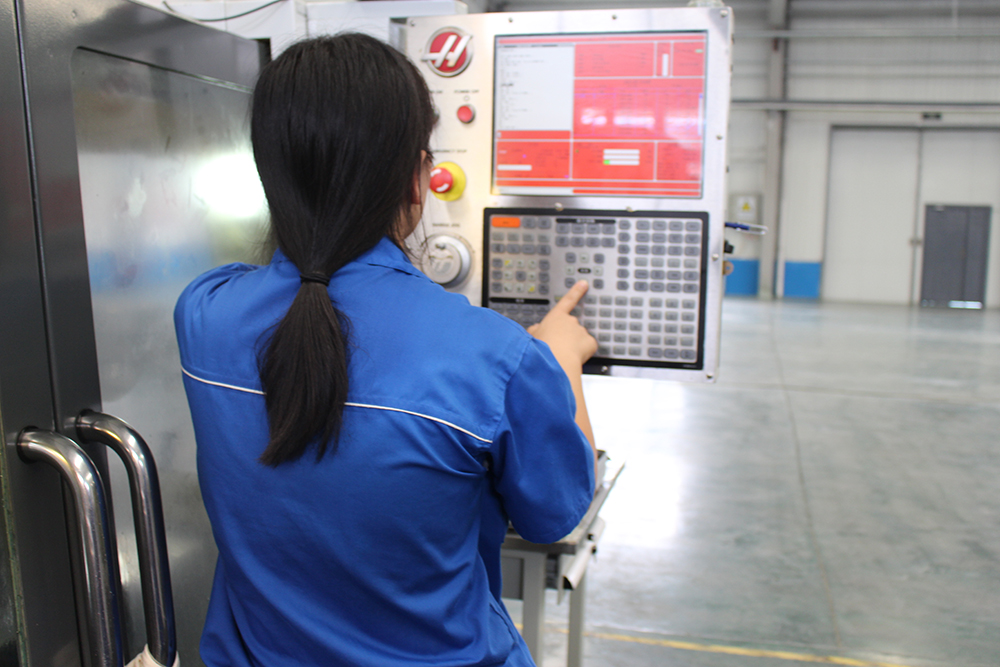
Complex geometries, such as the flute structures of our Flexible Reamers and the threads of cannulated bone screws, are manufactured via automated 5-axis Swiss-type lathe machines. This maintains tolerances down to 0.005mm.
To eliminate free iron and maximize natural chromium oxide barrier formation, every instrument undergoes acid passivation (nitric or citric bath) followed by electro-polishing. This prevents rust, pitting, and reduces biological adhesion in the sterile field.
For modern medical device procurement, navigating regulatory pathways is as crucial as the physical manufacturing of the device. At Shenzhen HUL Healthcare Technology (operating as Bopull Medical), our production operates under the strict mandate of GB/T42061-2022 idt ISO13485:2016 quality management system standard.
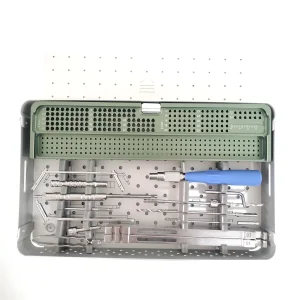
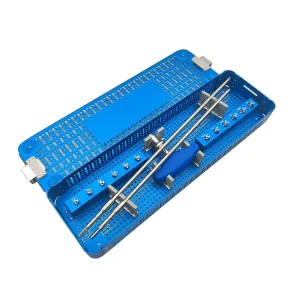
Whether you require localized labeling, custom sterilizable tray configurations, or direct registration dossiers for regulatory approval, our technical team offers seamless international cooperation:
Leveraging industrial clusters, sophisticated infrastructure, and scale economies to deliver medical-grade precision cost-effectively.
Operating in Shenzhen, China's premier high-tech hub, grants us direct access to precision electronics, high-grade steel mills, rapid prototyping, and surface-finishing facilities. This logistical ecosystem reduces supply-chain friction, leading to faster prototyping and production turnarounds.
By using automated manufacturing networks and maintaining a workforce of 301-500 skilled professionals, we keep production costs optimized. Our clients access premium products at 30-50% less cost compared to Western equivalents, without compromising material integrity.
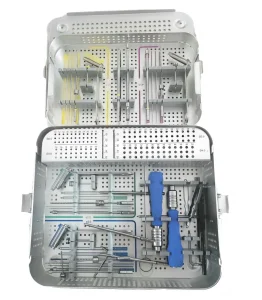
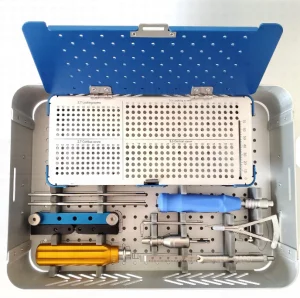
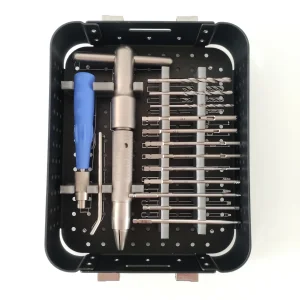
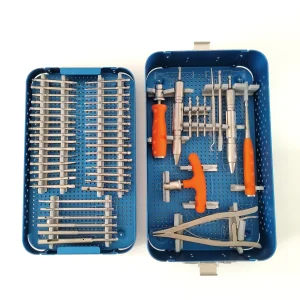
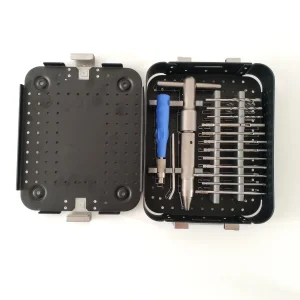
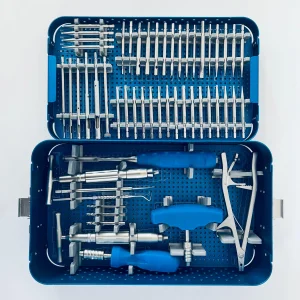
Our facilities accommodate sudden surges in demand. From high-precision custom orthopedic bone drills to complete instrument sterilization boxes, our factories scale production rapidly to fulfill large hospital tender demands.
As minimally invasive surgeries and advanced veterinary procedures grow, surgical instrument design must evolve accordingly.
The global healthcare sector demands highly specialized surgical kits that reduce intraoperative complications and shorten surgical time. In response, modern design trends emphasize:
Our product lines serve complex human orthopedics and specialized veterinary procedures.
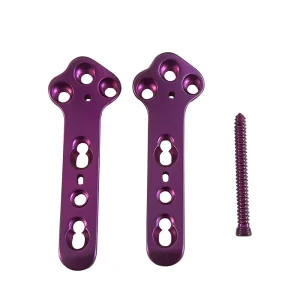
Specifically designed for canine veterinary care. The use of specialized ALPS Locking Plates and Screw Fixation Instrumentation reduces implant failure and promotes faster weight-bearing recovery in canine breeds recovering from cranial cruciate ligament ruptures.
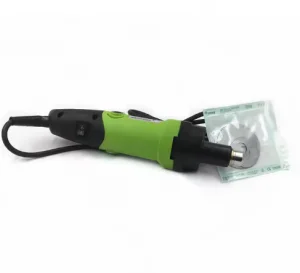
During revision surgeries, removing cold-welded or stripped locking screws is a complex challenge. Our electric and manual broken screw removal sets provide quick extraction, minimizing bone loss and trauma to the surrounding tissue.
Using flexible reamers allows surgeons to prepare the medullary canal for rod insertion during long bone fracture fixation, ensuring uniform diameter without heating the endosteal surface.
Operating under the global trade brand Bopull Medical, we deliver premium engineering to the medical sector.
Bopull Medical is strictly managed and operated in accordance with international laws, regulations, and quality standards. Our company has passed the GB/T42061-2022 idt ISO13485:2016 quality management system certification. Our focus on product quality has earned high praise across the orthopedic device manufacturing sector.
By employing advanced machinery, maintaining high-precision testing apparatus, and supporting a workforce of 301-500 employees, our factory combines dynamic innovation with strict quality control. We supply distributors, hospitals, and OEM partners worldwide, generating an annual export revenue of US$1 Million - US$2.5 Million.
Technical and regulatory answers regarding our surgical product manufacturing processes and international procurement.
 HUL Healthcare Limited