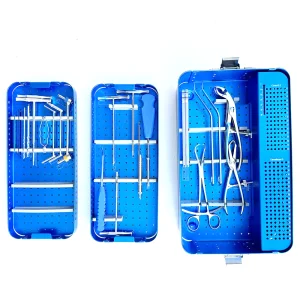
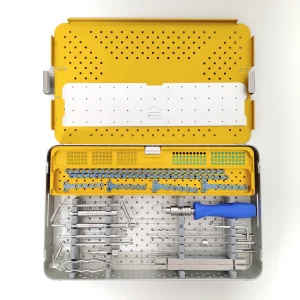
Explore our highly-engineered medical devices and precision surgical instrumentation built in compliance with ISO 13485 standards.
Analyzing clinical efficacy, polymer chemistry developments, and skin-barrier interaction in modern operative environments.
The progression of medical adhesives relies heavily on pressure-sensitive adhesives (PSAs). We design surgical tapes using advanced hypoallergenic acrylate copolymers and medical-grade silicone gel formulations. These substrates guarantee balanced skin adhesion, reducing mechanical trauma during peel-back while preventing transepidermal water loss (TEWL).
High Moisture Vapor Transmission Rate (MVTR) is critical for preventing skin maceration. Modern non-woven and micro-perforated PE surgical tapes utilize laser micro-pore technology, allowing the epidermis to transpire naturally during long-duration surgeries, securing sterile barriers even under high perspiration scenarios.
Our upcoming research roadmap focuses on biodegradable raw substrates, replacing synthetic backings with corn-derived polylactic acid (PLA) and organic bamboo fibers. Additionally, we are testing color-responsive tapes that signal shifts in pH, alerting clinical staff of potential local surgical site infections (SSI).
Bridging high-performance surgical tapes and complex orthopedic configurations to streamline clinical workflows.
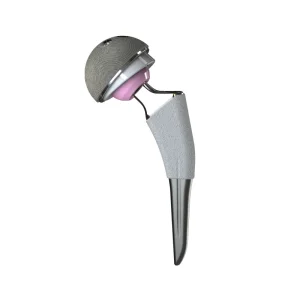
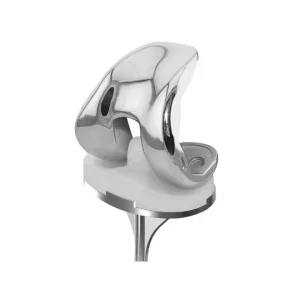
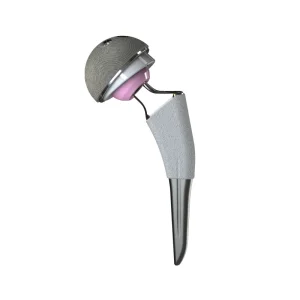
In modern operating environments, surgical consumables and hardware implants do not work in isolation. The integration between post-operative stabilization and biological dressing is critical. For instance, after executing a total hip system replacement or anchoring a distal tibia plate, the primary wound closing relies heavily on sterile biological barriers. Surgical tapes establish the defense system against surgical site infections, acting as the outermost stabilization layer for heavy dressings.
Our strategic manufacturing approach treats consumables as vital companions to orthopedics. By optimizing raw adhesive material structures and mechanical shear strengths, we provide clinical settings with a unified solution: high-grade biological implants stabilized with high-tenacity, low-irritation adhesive dressings.
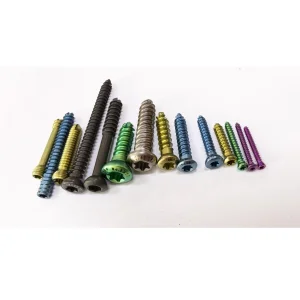
For trauma situations using tibia locking plates, our porous PE tapes provide high-strength initial dressing fixation under wet skin conditions.
Specialized animal skin anatomy requires tapes with high initial tack. Our non-woven medical tapes secure dressings even on short animal fur.
Medical-grade silicone tapes minimize skin stripping in pediatric, geriatric, and highly-sensitive skin types during prolonged healing phases.
High-tensile stretch tapes are configured to stabilize joint dressings under active load conditions, supporting dynamic patient recovery.
How our advanced production ecosystem guarantees cost efficiency, steady output, and international quality alignment.
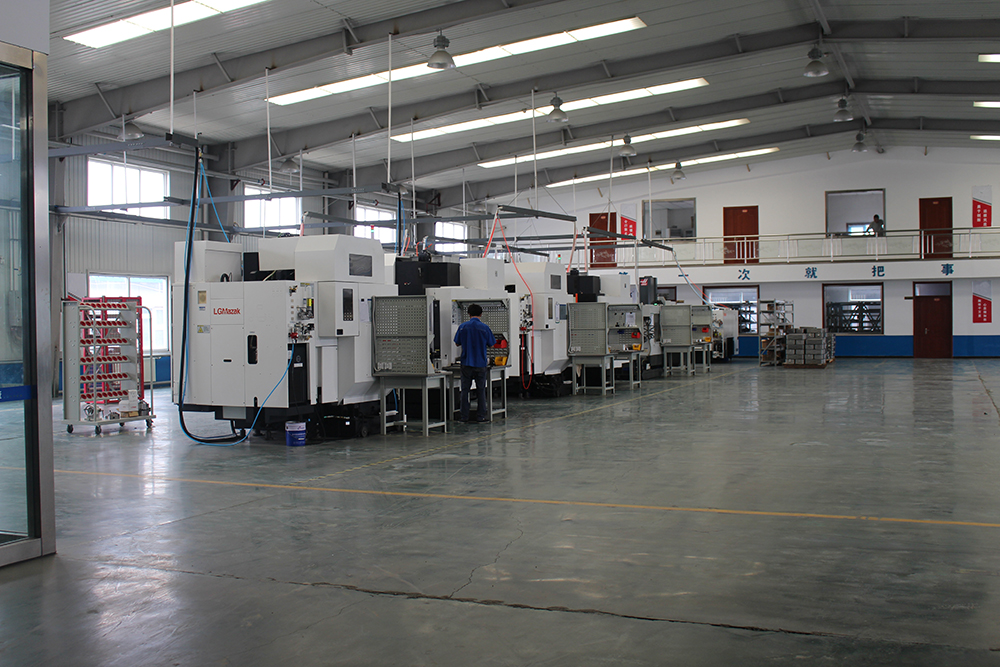
Operating under the brand Bopull Medical, our facilities strictly comply with international medical regulations and quality standards. Our production plant features fully automated coating systems, precise slitting machines, and class 100,000 cleanroom environments. This ensures that every roll of surgical tape or medical instrument is manufactured under sterile, temperature-controlled conditions.
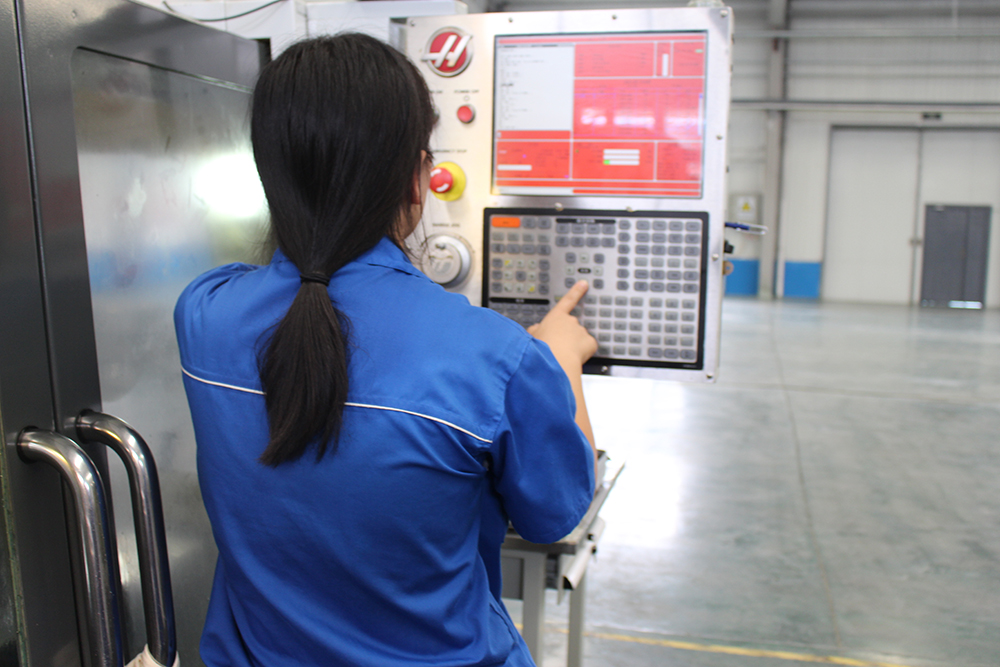
By automating the coating and slicing operations, we minimize manual contact, reducing contamination risks. Our state-of-the-art laboratory is equipped to conduct real-time peel strength testing, aging analysis, and residue checking, guaranteeing that our products withstand varying storage conditions across international shipping lanes.
| Company Name | Shenzhen HUL Healthcare Technology Co., Ltd. (Bopull Medical) |
| Standards & Quality | GB/T42061-2022 idt ISO13485:2016 Certification |
| Business Type | Manufacturer & Trading Company |
| Annual Revenue | US$1 Million - US$2.5 Million |
| Employee Count | 301 - 500 People |
| Key Locations | Beijing & Shenzhen, China |
Removing friction from the global healthcare supply chain with complete documentation and localization services.
We provide comprehensive registration dossiers, including ISO 13485 certification, CE markings, and compliance documentation. This ensures seamless custom clearance at major international ports and alignment with local health authorities.
From substrate selection (paper, silk, PE, non-woven) to custom branding, cores, and specialized packaging boxes, we adapt our output to suit local market demographics and hospital specifications.
Supported by our dual hubs in Beijing and Shenzhen, we coordinate multimodal logistics solutions. Whether handling LCL, FCL, or urgent airfreight, we optimize lead times to guarantee stable inventory levels.
Addressing the key technical, commercial, and operational concerns of global medical sourcing officers.
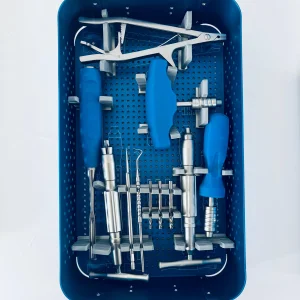
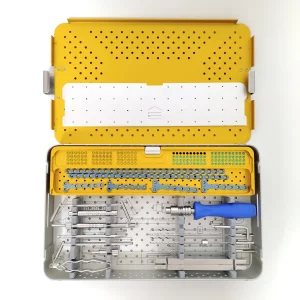
High-grade stainless steel and titanium surgical instruments engineered for clinical durability and precision.
A preview of our manufacturing precision, packaging lines, and logistics processing capability.
 HUL Healthcare Limited