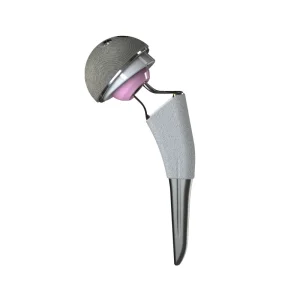
Explore our advanced catalog of CE-certified orthopedic components, spinal fixation systems, and surgical power devices manufactured to the highest clinical sterility standards.
In the modern clinical infrastructure, the demand for high-reliability sterile covers, camera drapes, and orthopedic device drapes has surged significantly. Operating theaters require absolute confidence in sterile field maintenance to mitigate the risk of Surgical Site Infections (SSIs), which contribute to billions of dollars in excess healthcare expenditures globally. Medical device importers, global distributors, and healthcare organizations are prioritizing procurement frameworks that balance technical performance, material reliability, and absolute compliance with international regulatory bodies.
Leading hospital procurement chains across the Americas, Europe, and Asia-Pacific have shifted towards consolidated supply chains. Rather than sourcing components independently, procurement boards seek strategic alliances with vertically integrated partners. This ensures that accessories, sterile covers, and specialty orthopedic surgical implants are manufactured, tested, and validated under cohesive quality management systems like ISO 13485.
Ensuring redundant manufacturing locations, robust material stockpiles, and reliable international logistics agreements to prevent sterile field product stockouts.
Rigorous validation documentation, biocompatibility certifications, and sterile field maintenance tests to meet international standards (FDA, CE, ISO).
Development of anti-static, low-glare, high-tactility, and high-tear-resistance polymer materials tailored for delicate robotic and optical surgical tools.
The execution of sterile protective measures extends far beyond simple polyethylene draping. Modern operations involve high-intensity equipment, including C-arm fluoroscopes, intraoperative MRI machines, robotic arms (such as DaVinci systems), and high-resolution surgical microscopes. Each of these components requires custom-tailored sterile covers designed to allow full physical range of motion, maximum visibility, and seamless communication across touch interfaces without compromising the sterile field.
By employing customized sterile cover systems, hospitals dramatically cut turnaround times between surgeries. Fast-drape technologies with intuitive directional markers allow nurses and technicians to cover complex equipment in seconds, reducing operational overhead and maximizing theater throughput.
| Material Type | Key Attributes | Clinical Application | Sterilization Compatibility |
|---|---|---|---|
| Linear Low-Density Polyethylene (LLDPE) | High tear strength, cost-effective, high transparency | General C-Arm drapes, microscope covers, probe covers | Ethylene Oxide (EO), Gamma Irradiation |
| Thermoplastic Polyurethane (TPU) | Extremely soft, high elasticity, tactile sensitivity | Robotic arm sleeves, surgical touch screens | EO, Electron Beam (E-Beam) |
| DuPont Tyvek® Laminates | Unmatched breathability, complete microbial barrier | High-durability orthopedic tool trays, packaging | EO, Gamma, Steam Autoclave |
Discover the manufacturing capability and quality standards driving Bopull Medical / HUL Healthcare.
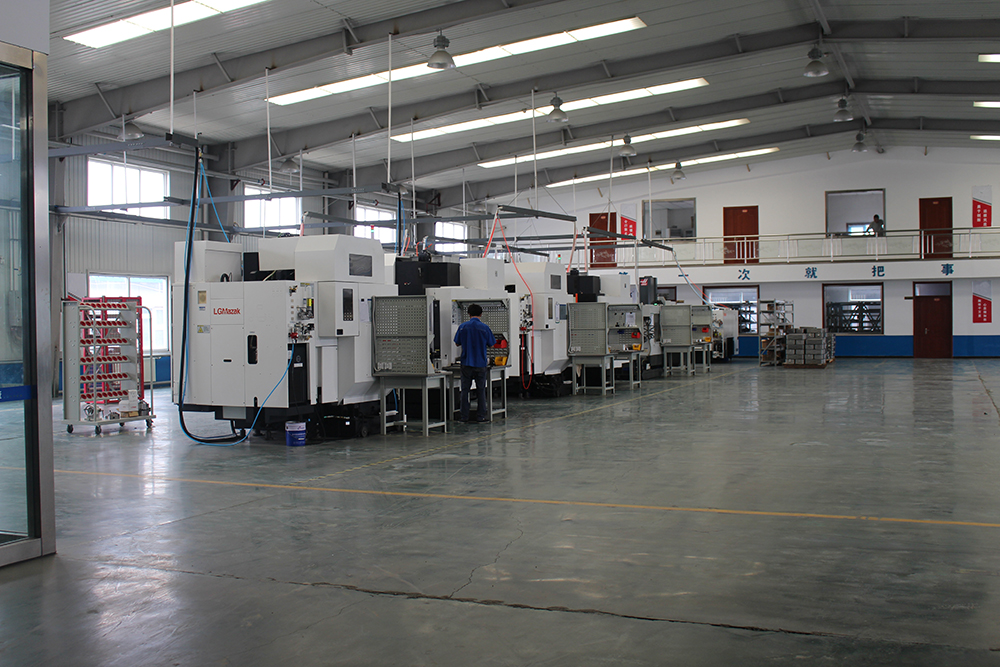
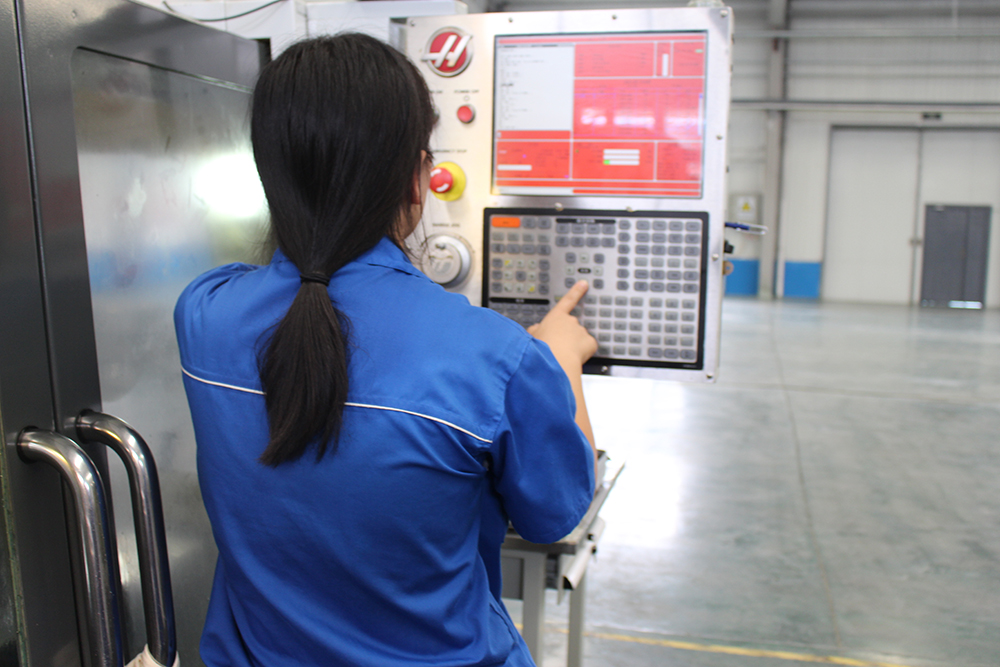
Shenzhen HUL Healthcare Technology Co., Ltd. (operating globally under Bopull Medical) has established a reputation for operating in strict alignment with international laws, regulations, and quality criteria. The company has passed the GB/T42061-2022 idt ISO13485:2016 quality management system international standard certification. This certification represents Bopull Medical's focus on maintaining stable production environments, cleanrooms, and technical processes to ensure zero-defect sterile outcomes.
With an annual revenue profile of US$1 Million - US$2.5 Million and a robust workforce of 301 - 500 professionals, the company continues to scale its operations. Located in Beijing, China, and operating as an experienced trading and manufacturing entity, they serve critical markets globally with a solid 34% seller reorder rate. This high customer retention indicates industry satisfaction, backed by an efficient customer response rate of 95.36% and an average response time of ≤3 hours.
The future of medical sterile covers revolves around smart polymers and eco-friendly manufacturing technologies. The industry is currently moving towards biodegradable, compostable, or highly recyclable medical drapes that do not sacrifice microbial performance. Standard polyethylene plastic drapes require hundreds of years to decompose, creating environmental pressure on hospital waste facilities.
Our technological roadmap focuses heavily on the development of multi-layered co-extruded films. By combining LLDPE with high-barrier polyolefins, we can produce films that are 30% thinner yet possess double the puncture and tear resistance. This reduction in material mass directly translates to a smaller environmental footprint, lower logistics costs, and superior flexibility for delicate operating room procedures.
In addition, the integration of anti-reflective coatings and anti-static additives guarantees that drapes covering visualization equipment (like robotic surgical screens or high-definition surgical cameras) do not distort the surgeon's view. Static electricity build-up in dry, positive-pressure OR suites can attract dust particles and debris. Modern anti-static layers prevent this, ensuring optimal visibility throughout lengthy clinical interventions.
Manufacturing sterile covers is only one half of the challenge; proving that they maintain sterility over long periods under varying transport conditions is the other. In accordance with ISO 11607 (Packaging for terminally sterilized medical devices), all sterile covers must undergo extensive shelf-life studies, transport simulations, and microbial challenge testing.
Before sterile covers can be imported into major global markets, they must pass strict regulatory reviews. In the European Union, products must comply with the Medical Device Regulation (MDR 2017/745), requiring detailed clinical evaluations and class classification reviews. In the United States, FDA 510(k) clearances ensure that the drapes are substantially equivalent to marketed sterile surgical barriers.
Shenzhen HUL Healthcare Technology Co., Ltd. remains committed to absolute validation. Every single batch of sterile covers undergoes strict batch testing, including bioburden analysis, sterility verification post-EO gas exposure, and residual EO gas level inspections, ensuring patient safety is never compromised.
Expert insights regarding the procurement, customization, and certification of global sterile covers and surgical instruments.
Explore our premium selection of sports medicine products, orthopedic plates, veterinary joint implants, and high-precision shaver blades.
 HUL Healthcare Limited